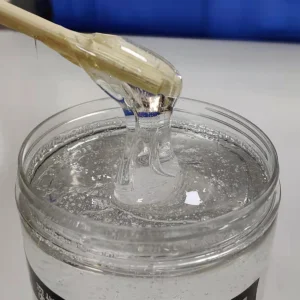


Immediate wholesale procurement availability directly from state-of-the-art Chinese synthesis plants. Explore verified batch properties, technical data sheets, and custom formulation options.
Industrial liquid latex compounds represent engineered colloidal dispersions of cis-1,4-polyisoprene polymer chains stabilized in aqueous matrices. Demystifying its crosslinking mechanisms unlocks unprecedented dimensional precision and cycle longevity.
Pre-vulcanized molding latex features crosslinking activators integrated directly at the colloidal stage, initiating gradual room-temperature film coalescence without requiring high-temperature oven cycles. For complex dimensional reproductions, vulcanizing agents like sulfur micro-dispersions, zinc diethyldithiocarbamate (ZDEC), and zinc oxide (ZnO) establish durable covalent monosulfide and disulfide linkages, guaranteeing elongation limits exceeding 800%.
Wholesale molding efficacy hinges upon Total Solids Content (TSC) and Dry Rubber Content (DRC). Low-ammonia centrifugation yields a pristine 61.5% to 63.0% solids spectrum, minimizing dehydration shrinkage to under 1.2%. High solids concentrations avoid excessive layer accumulation during multi-brush applications, significantly slashing cure cycle overheads in massive casting applications.
Native latex features near-Newtonian rheology, predisposing it to pooling on vertical reliefs. Introducing associative polyurethane or sodium polyacrylate thickeners induces a shear-thinning thixotropic profile. This allows effortless spraying and brushing at high shear, transitioning rapidly into zero-sag films on steep mold contours and high-relief negative matrices.
| Physical / Chemical Metric | High-Ammonia Latex (HA) | Low-Ammonia Compound (LA-TZ) | Synthetic L-XNBR Reinforced | Target Testing Standard |
|---|---|---|---|---|
| Dry Rubber Content (DRC, %) | ≥ 60.0% | ≥ 61.5% | ≥ 64.0% | ASTM D1076 / ISO 126 |
| Total Solids Content (TSC, %) | 61.5% - 62.5% | 62.8% - 63.8% | 65.2% - 67.0% | ISO 124:2014 |
| Alkalinity as Ammonia (NH₃, %) | 0.65% - 0.75% | ≤ 0.20% (TMTD/ZnO stabilized) | < 0.05% (pH 8.5 buffered) | ASTM D1076 |
| Tensile Strength (MPa) | 24.5 - 28.0 MPa | 26.0 - 30.5 MPa | 32.0 - 36.0 MPa | ASTM D412 (Dumbbell) |
| Ultimate Elongation (%) | 750% - 850% | 800% - 900% | 680% - 750% | ASTM D412 Type C |
| Brookfield Viscosity (mPa·s, 25°C) | 40 - 80 (Unthickened) | 60 - 120 (Unthickened) | 1200 - 3500 (Adjustable) | LV Spindle 2 @ 30 RPM |
YANXA capitalizes on mature chemical upstream clusters in China to deliver an unrivaled price-to-performance matrix, strict ISO compliance, and seamless dangerous goods handling across global maritime corridors.
Proximity to regional petrochemical infrastructure guarantees consistent availability of synthetic comonomers (such as carboxylated butadiene, acrylonitrile, and styrene-butadiene rubber). This upstream integration decouples pricing from wild raw latex market surges.
Our domestic facilities utilize 20,000-liter computer-controlled reactors featuring dual planetary dispersion, in-line particle size tracking, and inert argon padding. This eliminates batch-to-batch variation in modulus, viscosity, and curing curves.
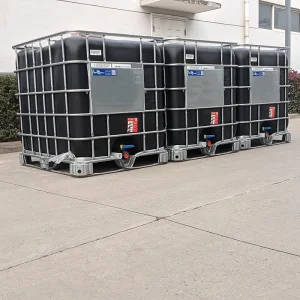
Lower synthesis costs combined with efficient bulk containerization (1,000L IBC totes and 24,000L Flexitanks) grant wholesale distributors an average 22% to 38% cost reduction compared to European or North American compounders without compromising performance.
Direct intermodal rail-and-port links to Qingdao, Ningbo, and Shanghai enable compliant dangerous goods (DG) and non-DG handling under IMDG regulations, ensuring rapid customs clearances and steady oceanic transit times worldwide.
Emerging regulatory frameworks, ultra-low VOC imperatives, and hybrid elastomer matrices redefine international demand across industrial casting and artistic replication.
Conventional high-ammonia latex exposes workers to caustic fumes and triggers severe skin sensitization. The industry is rapidly pivoting to low-ammonia zinc oxide (LA-ZnO) and enzymatically modified natural rubber (ENR). These formulations curb workplace emissions by up to 85% while meeting strict occupational exposure limits in the EU and North America.
Pure natural latex degrades under aromatic hydrocarbon solvents, aggressive resins, and cyclic ozone exposure. Compounding cis-polyisoprene with liquid carboxylated nitrile rubber (L-XNBR) or hydroxyl-terminated polybutadiene (HTPB) yields composite molds with up to three times greater tear propagation resistance and enhanced resistance to styrene resins.
Automated casting lines require high-solids emulsions that cure quickly without surface crusting. Advanced chemical complexes with thermal-sensitizing coagulants (like organosiloxane emulsions) enable uniform wall thickness in robotic dipping, cutting process times from 48 hours to under 4 hours.
From micro-textured architectural facade duplication to cinema-grade prosthetics, customized compound formulations match the unique chemical and physical demands of diverse curing environments.
Masonry casting requires robust resistance against highly alkaline Portland cement (pH 12.5–13.5). Our reinforced latex compounds feature added non-ionic surfactants that prevent alkaline destabilization and premature film embrittlement, easily withstanding more than 200 high-abrasion stripping cycles.
Special effects call for high-modulus elasticity and feather-light film transitions. Our low-odor, skin-compatible dipping latex cures into a flexible skin that transfers fine sub-micron pores, hair textures, and lifelike skin dynamics without tearing during demolding.
Preserving fragile antiquities and detailed historical monuments requires non-staining, chemically neutral formulations. Our sulfur-free, ultra-filtered pre-vulcanized latex releases effortlessly without stripping fragile patinas, stone crumb, or historical paints.
Thermoset resin systems release significant exothermic heat (often topping 90°C) and corrosive free styrene monomers. By crosslinking our natural latex with specialized heat stabilizers, the elastomer matrix stays elastic, preventing mold warpage and burning.
YANXA offers transparent, volume-tiered pricing. Rates are calibrated directly against international rubber indices, freight movements, and custom stabilization needs.
| Elastomer Grade / System | Standard Packaging | MOQ | Tier 1 Price (FOB Base) | Tier 2 Bulk Price (>20 MT) | Lead Time |
|---|---|---|---|---|---|
| Pre-Vulcanized Natural Latex (60% DRC) | 200 kg HDPE Drum / 1000L IBC | 1 Metric Ton | $1,850 – $2,100 / MT | $1,620 – $1,800 / MT | 7 - 10 Business Days |
| Low-Ammonia Mask & Prosthetic Compound | 25 kg Carboy / 200 kg Drum | 500 Kilograms | $2,200 – $2,450 / MT | $1,950 – $2,150 / MT | 5 - 8 Business Days |
| High-Solids Brush-On Latex (Thixotropic) | 200 kg Drum / 1000L IBC | 2 Metric Tons | $2,050 – $2,300 / MT | $1,800 – $1,980 / MT | 10 - 12 Business Days |
| L-XNBR Synthetic Rubber Fortified | 1000L IBC / Flexitank | 5 Metric Tons | $2,700 – $3,150 / MT | $2,450 – $2,800 / MT | 14 - 18 Business Days |
| Ultra-Elastic Concrete Casting Compound | 200 kg Steel/HDPE Drum | 1 Metric Ton | $1,950 – $2,250 / MT | $1,720 – $1,890 / MT | 7 - 10 Business Days |
Adjusting properties with silane coupling agents, flame retardants, or aluminum flake fillers is fully supported. Custom viscosity profiling (up to 40,000 cps) is confirmed on every batch Certificate of Analysis (COA).
Our experienced export desk manages UN-rated packaging, GHS labeling, and full IMDG/IATA hazardous material documentation, ensuring completely compliant customs handoffs.
Each production run undergoes rigorous pre-shipment tests—covering solid fraction stability, ash content, volatility, and mechanical limits. Third-party testing by SGS or Intertek is available upon request.
Straightforward answers addressing key engineering concerns, compound properties, storage limitations, and global procurement procedures.
Complete your formulation and synthesis matrix with specialized polymers, metal modifiers, and ultrapure process gases available from our verified inventory.