Explore high-purity metal powders, reactive polyethers, and cross-linking agents deployed in severe hydrostatic pond lining and chemical manufacturing applications.
From fragile sheets to monolithic, chemically cross-linked liquid elastomer barriers: decoding the paradigm shift across industrial containment facilities.
Traditional preformed sheet geomembranes such as HDPE and vulcanized EPDM rely heavily on thermal wedge or solvent-welded seams. In civil engineering statistics, over 84% of hydraulic liner failures occur directly along field seams caused by uneven thermal application or mechanical shear stress. Liquid rubber cures in-situ to produce a seamless, fully bonded barrier without weak joint interfaces.
Commercial aquaculture systems and decorative koi ponds require strictly non-leaching chemistries. Conventional coal-tar, aromatic polyurethanes, and solvent-cut bituminous coatings emit toxic phenols and volatile organic compounds (VOCs). Modern pond-grade liquid rubber is formulated with waterborne modified bitumen emulsions or prepolymers that are entirely fish-safe and plant-safe once fully cured.
Ponds constructed on earthen substrates, reinforced concrete, or geotextile-lined gravel beds experience relentless ground subsidence, freeze-thaw cycles, and seismic movement. Utilizing advanced polymers such as CTBN and hydroxy-terminated liquid rubbers, liquid pond liners achieve tensile elongation capacities exceeding 800% to 1100%, effectively bridging moving substrate fissures up to 6mm wide.
Strategic purchasing criteria for municipal water retention, tailings containment, and high-density industrial fish farms.
Factory quotes must be audited based on Dry Film Thickness (DFT) versus Wet Film Thickness (WFT). Low-cost formulations often contain under 40% solids, resulting in excessive volume shrinkage and pinholing during ambient drying.
Specifying pure elastomeric bitumen vs. epoxy-modified polyurethane vs. modified polybutadiene (EPB) directly affects hydrolytic stability, UV resistance, and chemical compatibility against agricultural fertilizers and bio-waste.
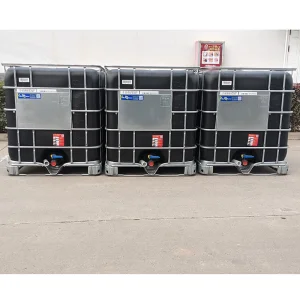
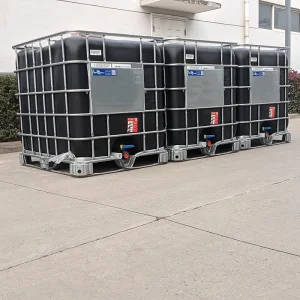
Quotes scale with raw polymer monomers, functional terminated groups, and antioxidant package loadings. Volume factory pricing typically operates on tiers for 200L drums, 1000L IBC totes, or bulk ISO-container delivery schemes.
Procuring contractors must designate application gear—high-pressure airless spray rigs require shear-thinning thixotropic properties (2,000–5,000 cPs), whereas squeegee or roller applications necessitate 15,000–35,000 cPs.
| Evaluation Parameter | Standard EPDM Sheet | HDPE Geomembrane | Industrial Liquid Rubber (YANXA System) |
|---|---|---|---|
| Seamless Continuous Cure | No (Mechanical/Tape joints) | No (Extruded/Thermal seams) | Yes (100% Monolithic envelope) |
| Tensile Elongation Capacity | 300% – 450% | 12% – 18% (Yield) | 850% – 1200% (Elastic recovery) |
| Penetration Sealing (Pipes, Steps) | Requires boots, clamps & caulk | Requires fabricated extrusion welds | Direct brush/spray cast encapsulation |
| Toxicity & Biological Leaching | Varies by plasticizer package | Inert, but rigid | Zero VOC, Fish-Safe (Certified OECD 203) |
| Adhesion to Concrete/Porous Rock | Zero direct mechanical bond | Zero direct mechanical bond | >2.2 MPa (Substrate destructive failure) |
Deep-tier chemical synthesis delivering unyielding hydrolytic stability under permanent hydro-static pressure.
Integrating Carboxyl Terminated Nitrile Butadiene Rubber (CTBN) or Hydroxyl Terminated Butadiene Rubber (HTBN) into liquid elastomeric compounds acts as a dedicated toughening and flexibility agent. It significantly diminishes micro-cracking during hydrostatic shock, prevents premature embrittlement, and boosts low-temperature flexibility down to -45°C.
Epoxy-modified liquid rubbers provide simultaneous benefits: the elastic recovery of an unsaturated polymer backbone coupled with the aggressive substrate adhesion of epoxy functional groups. This makes the coating self-priming over moist masonry, shotcrete, porous sandstone, and structural steel drainage conduits.
State-of-the-art dual-component liquid systems use specialized latent polyethers or latent amine cross-linkers that activate upon contact with atmospheric moisture or catalyst dosing. This eliminates blistering caused by internal vapor release and allows rapid water submersion testing within 24 to 48 hours of spray installation.
Strict conformity with international ecological containment, aquaculture safety, and dangerous goods transport guidelines.
Manufactured to meet stringent zero-toxicity limits (OECD 203 testing on trout and daphnia), ensuring zero release of heavy metals, phthalates, or bioaccumulative polycyclic aromatic hydrocarbons into freshwater ecosystems.
Every single batch undergoes testing for rheological consistency, Brookfield viscosity, solids content, cure rate, tensile strength, and cold temperature ductility. Retained samples are vaulted for 24 months to support full supply chain traceability.
Shipments leave with an authentic batch Certificate of Analysis (COA), 16-section GHS-compliant Safety Data Sheets (SDS), Technical Data Sheets (TDS), and applicable IMDG / IATA non-hazardous/hazardous declarations.
Exporting materials to over 60 countries across Southeast Asia, the Middle East, the Americas, and Europe with custom-palletized drums, UV-protected IBC containers, and climate-controlled freight when required.
Essential answers for engineers, distributors, and procurement managers evaluating factory-direct shipments.
A standard 200-liter drum will cover approximately 100 to 130 square meters at a recommended dry film thickness (DFT) of 1.2 mm to 1.5 mm across two coats, depending on substrate porosity and geotextile absorption characteristics.
For earthen ponds, best engineering practice requires installing a non-woven polypropylene geotextile fabric (minimum 200 g/m²) over compacted earth first. The liquid rubber is then spray-applied onto the geotextile, impregnating it to form a monolithic, root-resistant composite barrier.
Formulations intended for exposed pond edges or shallow water features are enriched with carbon black, hindered amine light stabilizers (HALS), and UV blockers, resisting photodegradation for more than 20–25 years without hardening or surface chalking.
Under standard ambient conditions (25°C, 50% relative humidity), skin formation occurs within 2 to 4 hours. Complete chemical vulcanization throughout the cross-section requires 48 to 72 hours before full hydrostatic water filling is initiated.
Yes. By altering nitrile polymer content (such as higher acrylonitrile concentrations in CTBN/HTBN polymers) or adding specialized vinyl-terminated polybutadiene, we provide specialized coatings resistant to mild acids, caustic washdown chemicals, and high-salinity marine farming basins.
Available in 20L pails, 200L steel/plastic drums, and 1000L IBC totes. Shelf life is guaranteed for 12 months when stored in sealed original containers away from direct heat and freezing conditions (recommended storage: 5°C to 30°C).
Comprehensive portfolio of functional polybutadienes, nitrile prepolymers, and complementary specialty chemical supplies available for wholesale export.