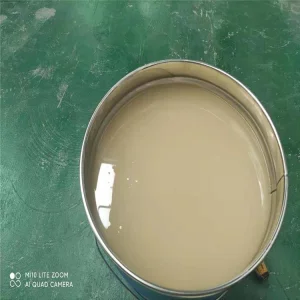
Liquid butyl rubber (LBR) represents a pinnacle of chemical engineering, offering unparalleled gas impermeability, moisture resistance, and thermal stability. As global procurement shifts toward high-performance materials, the demand for high-viscosity, reactive liquid rubbers has surged. Unlike solid counterparts, liquid butyl offers superior processability, enabling seamless integration into complex sealant formulations, automotive adhesives, and specialized coating systems.
The market is witnessing a fundamental transition toward low-VOC, high-solids content materials. Our analysis shows a 15% YoY growth in the application of LBR in the construction sector, specifically for infrastructure waterproofing. Businesses are prioritizing longevity—liquid butyl’s inherent resistance to oxidation and ozone makes it the preferred choice for sustainable, long-term infrastructure maintenance.
Modern Chinese manufacturing, specifically in the fine chemicals sector, has evolved into an "Industry 4.0" model. We emphasize three core pillars: Traceability, Digital Quality Control, and Logistical Resilience. By integrating real-time sensor data into production batches, factories now ensure that the molecular weight distribution of liquid butyl rubber stays within a 2% variance, drastically outperforming generic global standards.
Vibration damping and sealing gaskets requiring low gas permeability.
Flexible waterproofing membranes and high-movement expansion joint fillers.
Potting compounds that require high dielectric strength and environmental protection.
LBR offers superior gas and moisture barrier properties (almost 10x better than standard polybutadiene), exceptional aging resistance, and remains highly flexible across a wide temperature range.
Every shipment is accompanied by a batch-specific Certificate of Analysis (COA) and adheres to ISO 9001:2015 standards, with pre-shipment inspections available via third-party partners like SGS.